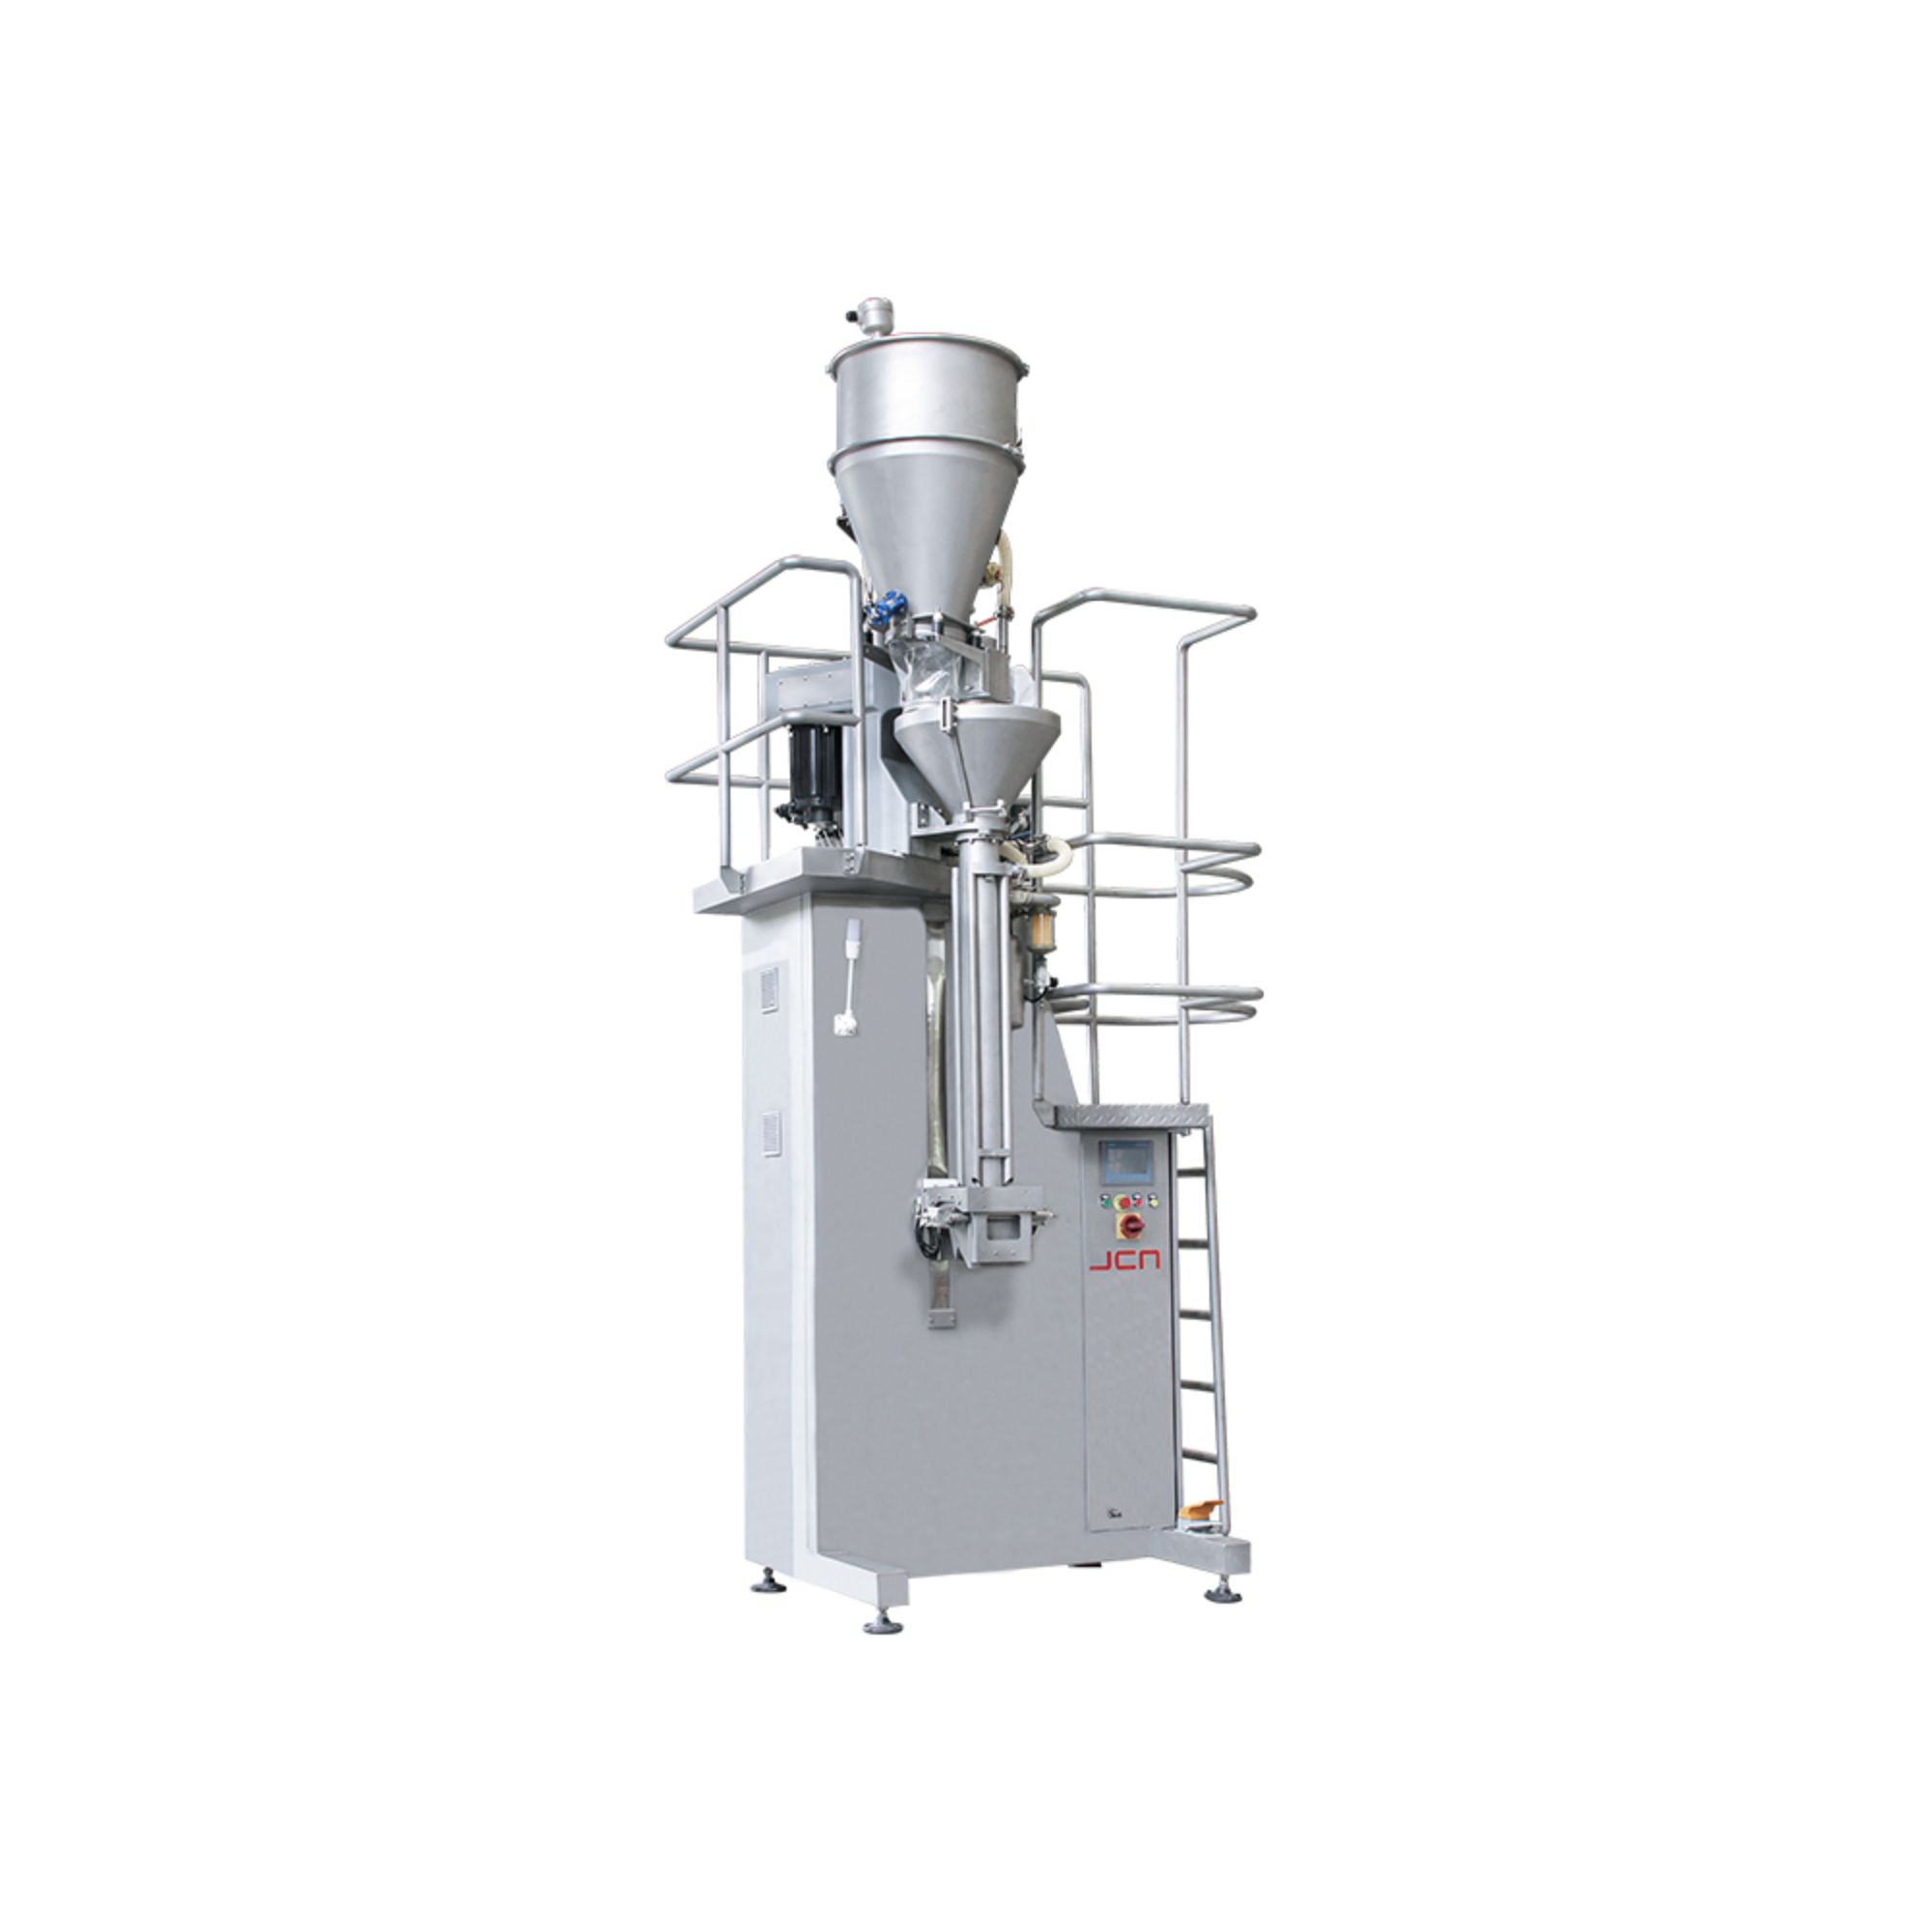
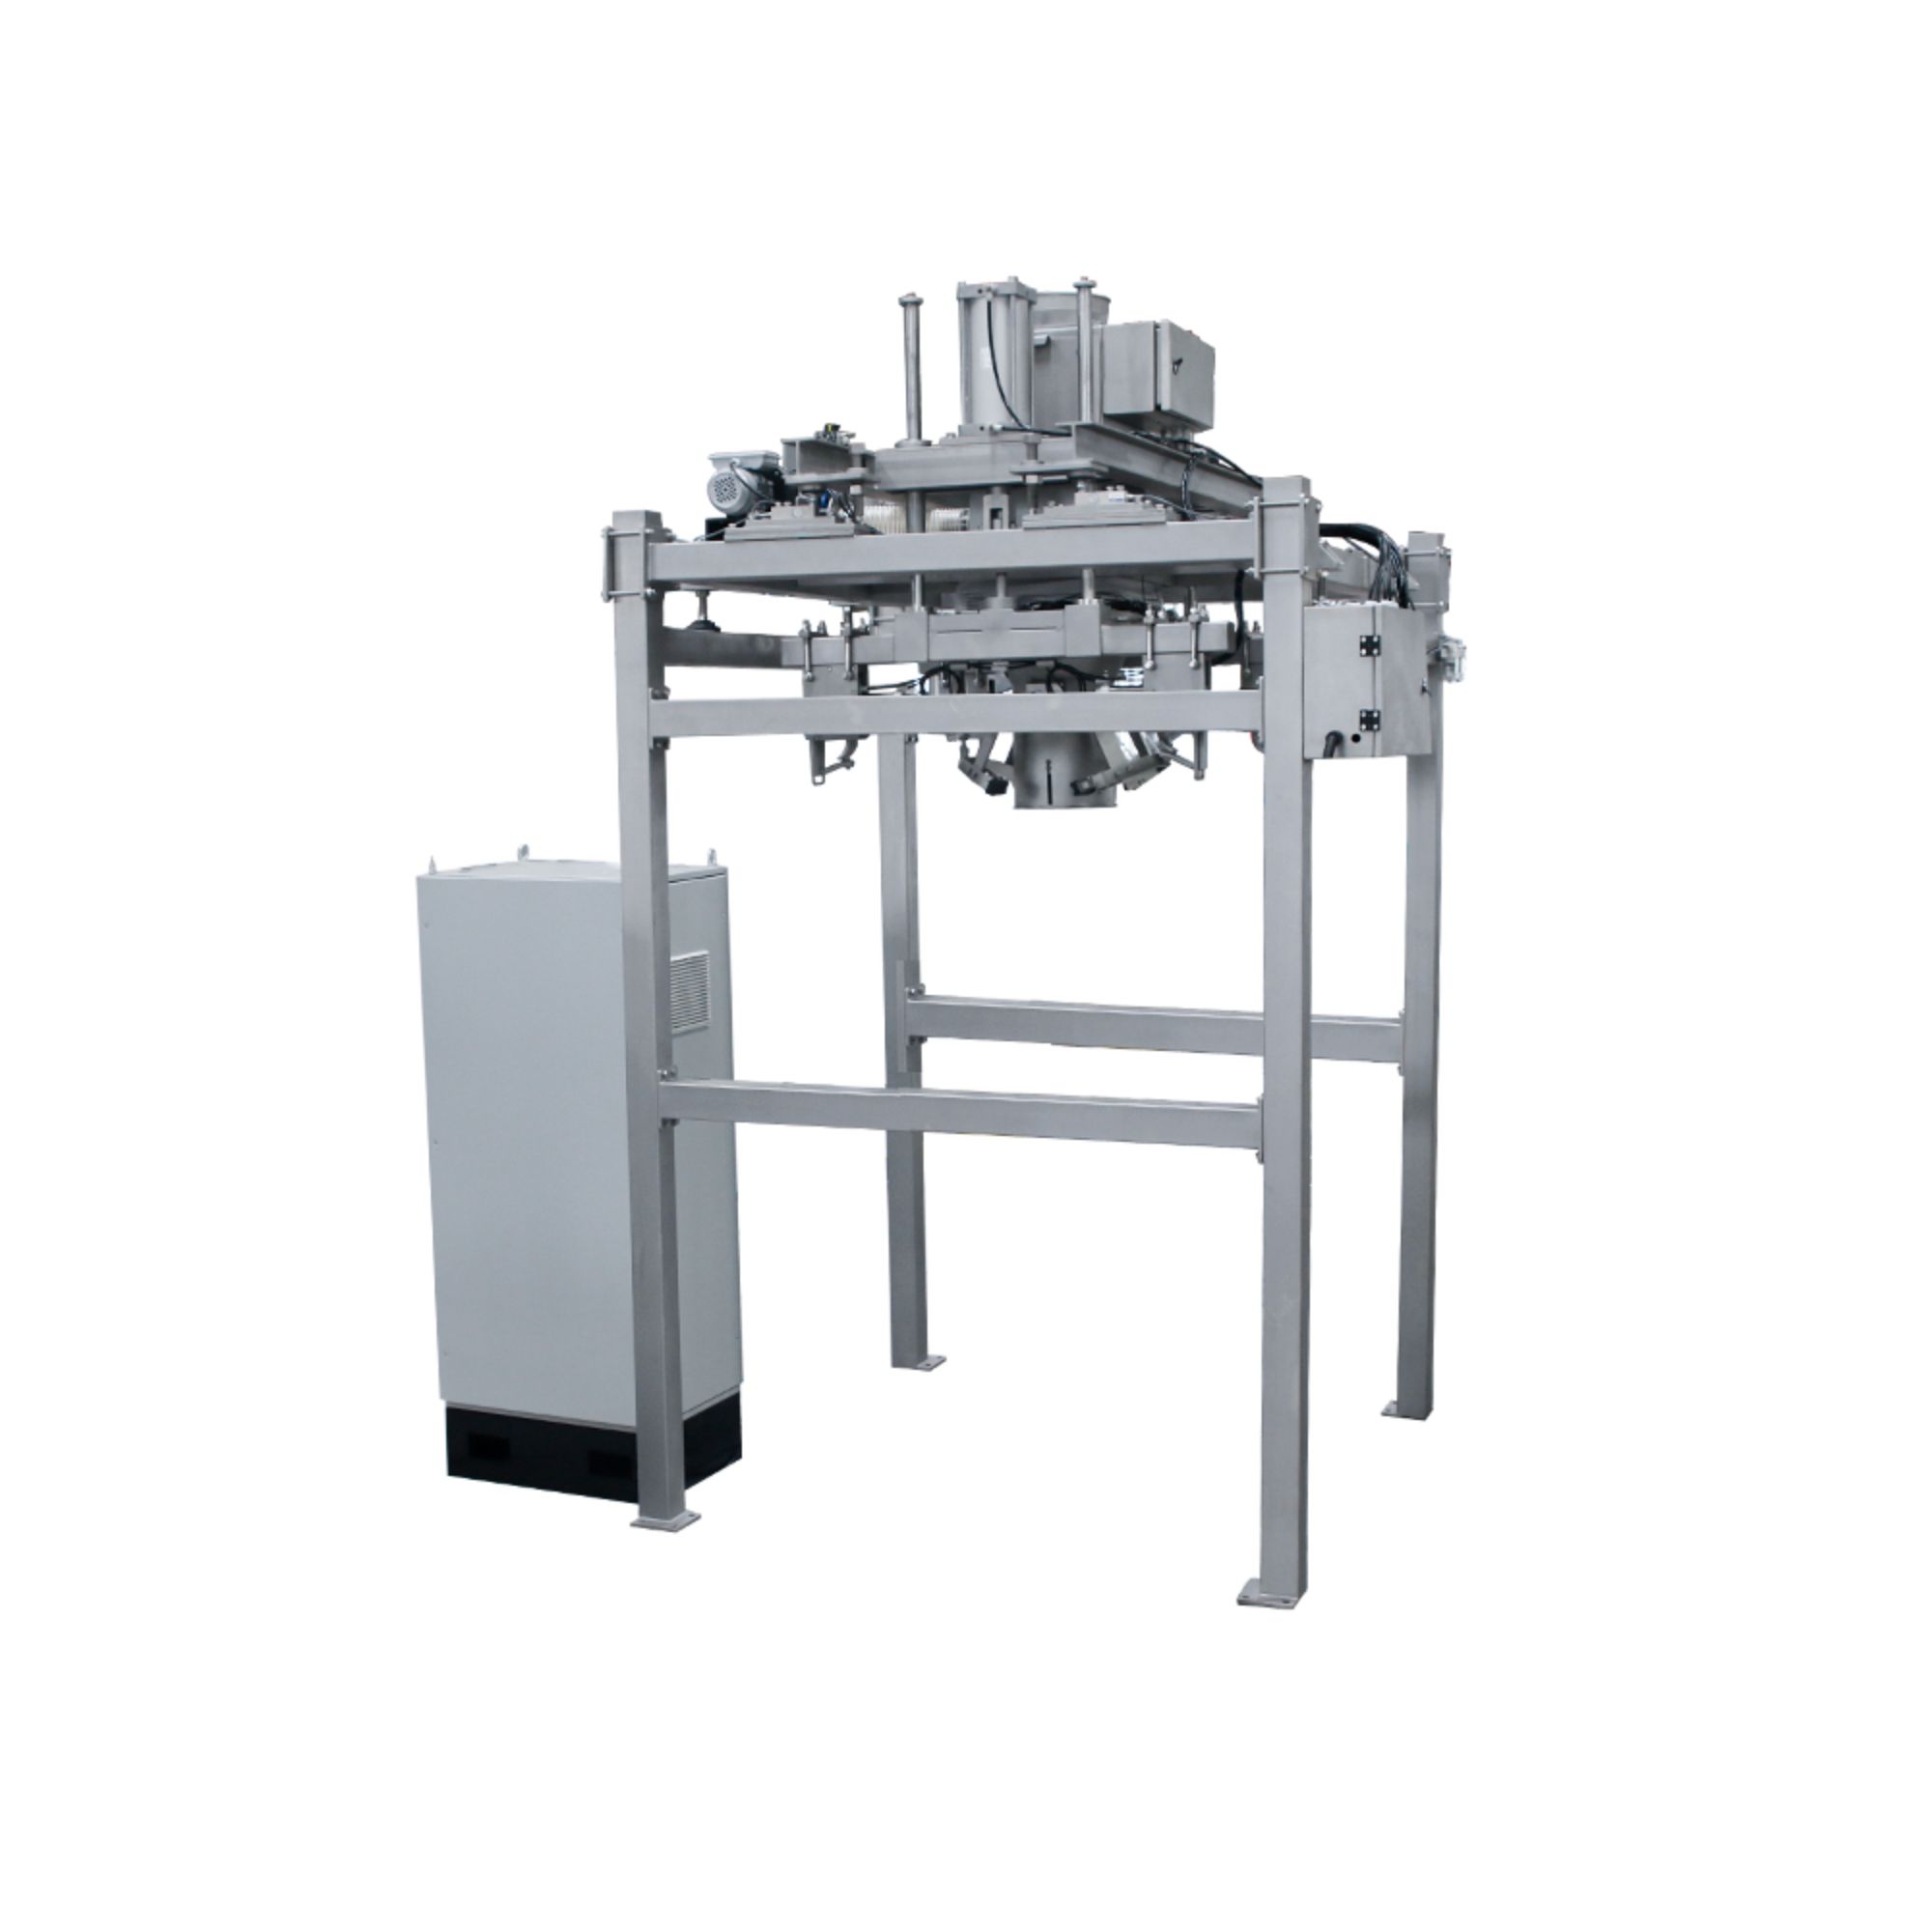
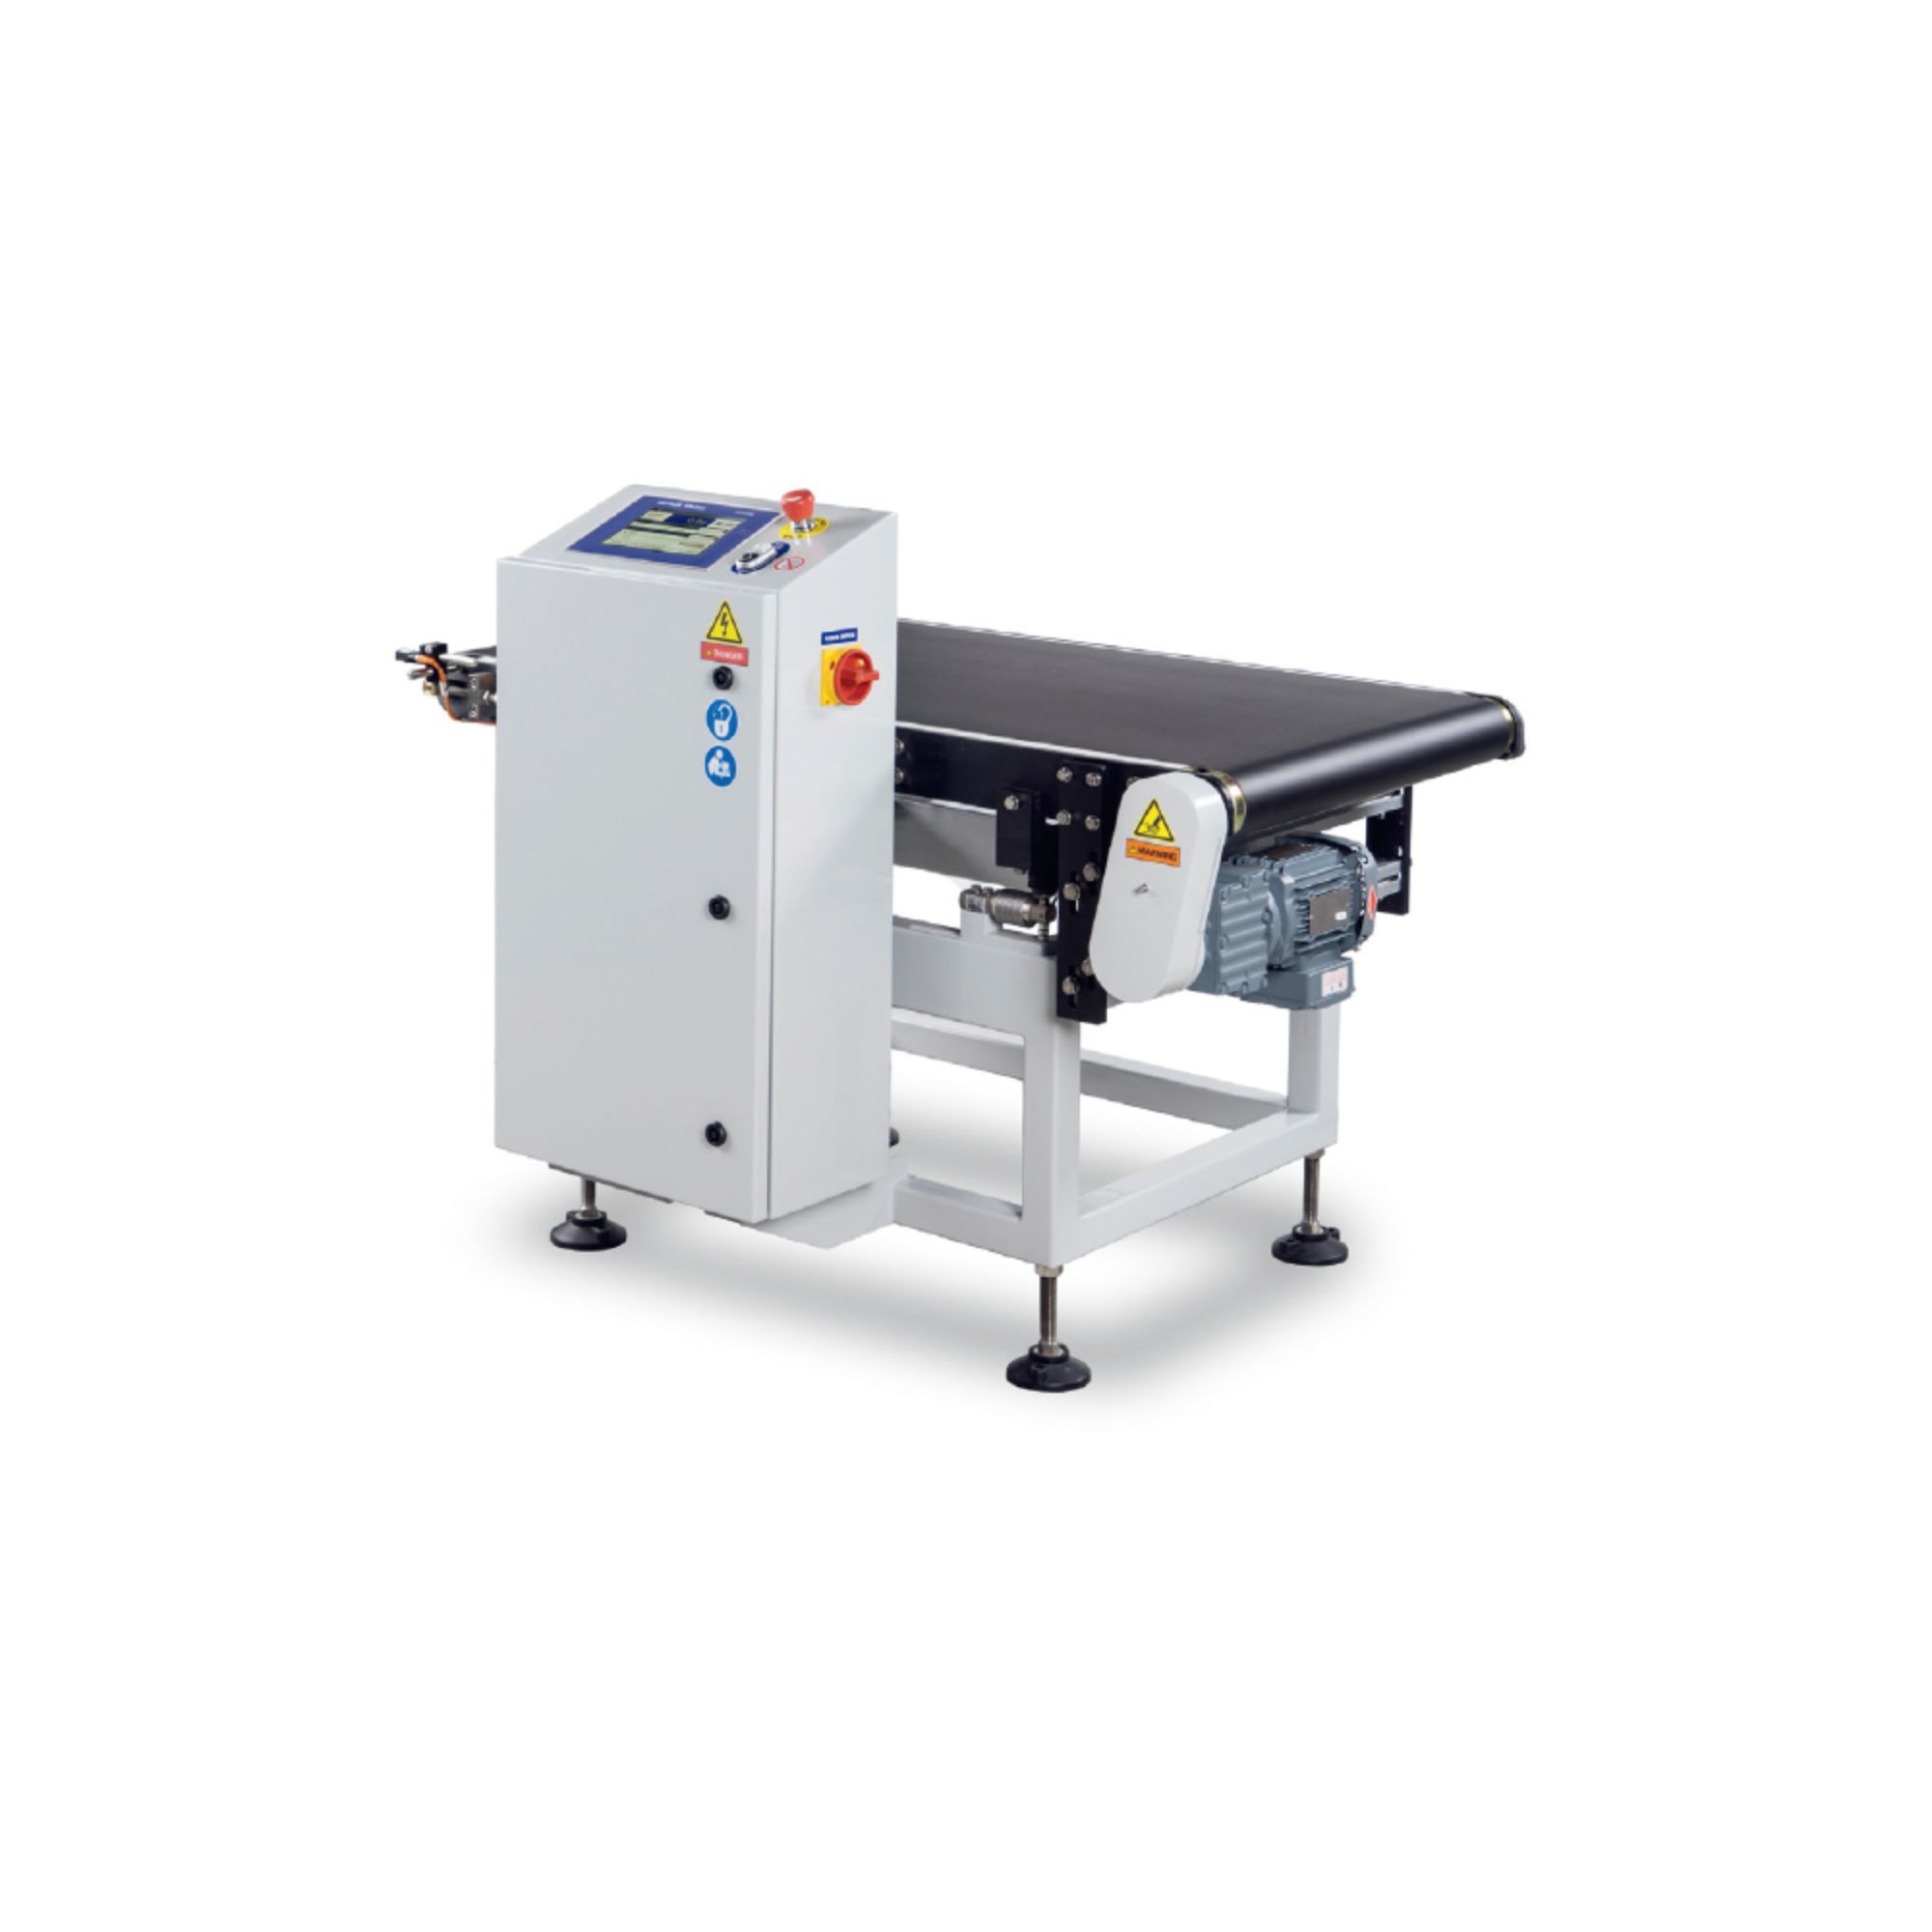
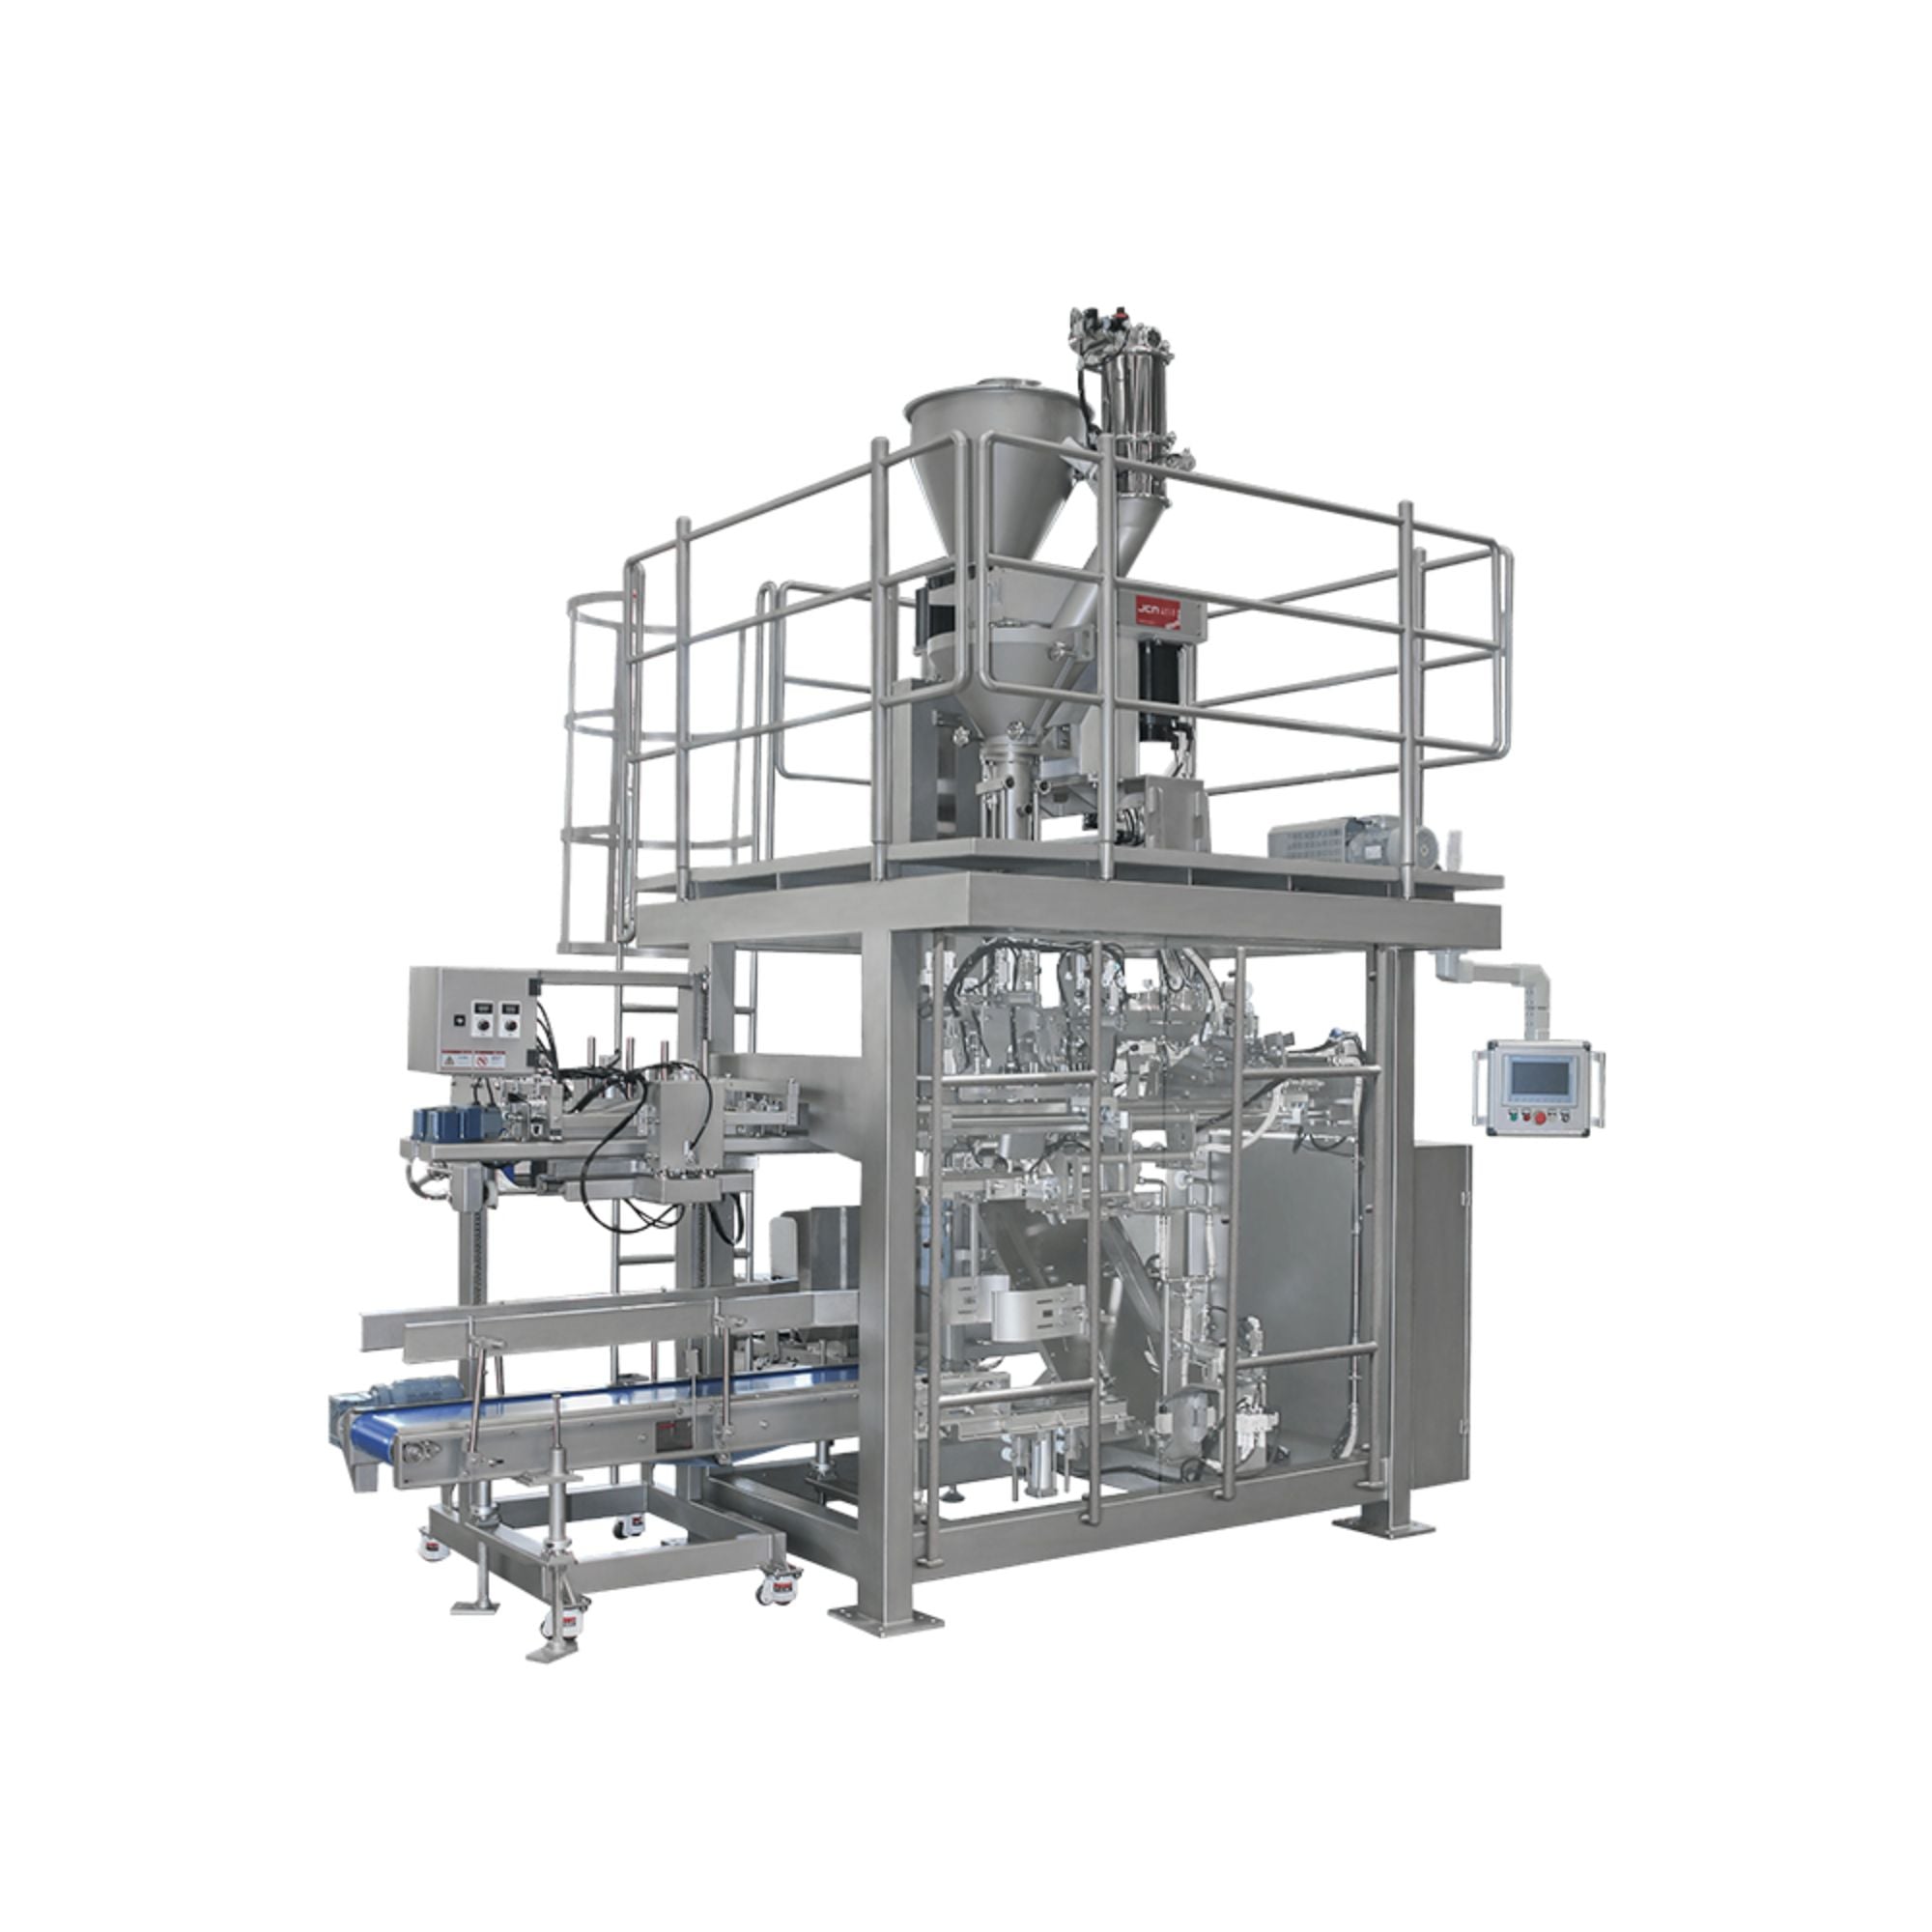
Big bag unloaders are essential pieces of equipment designed to facilitate the efficient handling and transfer of bulk powder materials from large bags into processing systems. For B2B buyers, such as purchasing managers and engineers, understanding the intricacies of selecting, installing, and operating these systems is crucial. This article will address common installation challenges, explore applications across industries, discuss cost factors for bulk purchases, and outline essential features to consider when sourcing big bag unloaders.
Installing a big bag unloader can present various challenges that may hinder its efficiency. One common issue is inadequate space for maneuvering and positioning the equipment. Before installation, it is vital to assess the available space and ensure that the unloader can be easily accessed for maintenance and operation. If space is restricted, consider a compact model or one that can be customized to fit your operational layout.
Another frequent challenge arises from improper alignment with existing processing equipment. Misalignment can lead to material blockages or inefficient transfers. To mitigate this issue, conduct thorough measurements and possibly engage in a pre-installation review with the manufacturer. This will help confirm that the unloader's specifications match your facility's requirements.
Additionally, proper electrical and pneumatic connections are critical for the operability of big bag unloaders. Ensure that your facility's power supply and air systems meet the specifications of the unloader. Consulting with the manufacturer or a qualified technician during installation can help address these electrical and pneumatic requirements effectively.
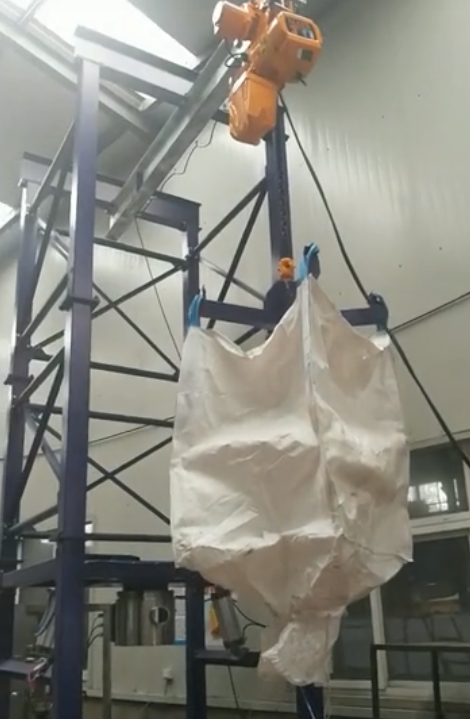
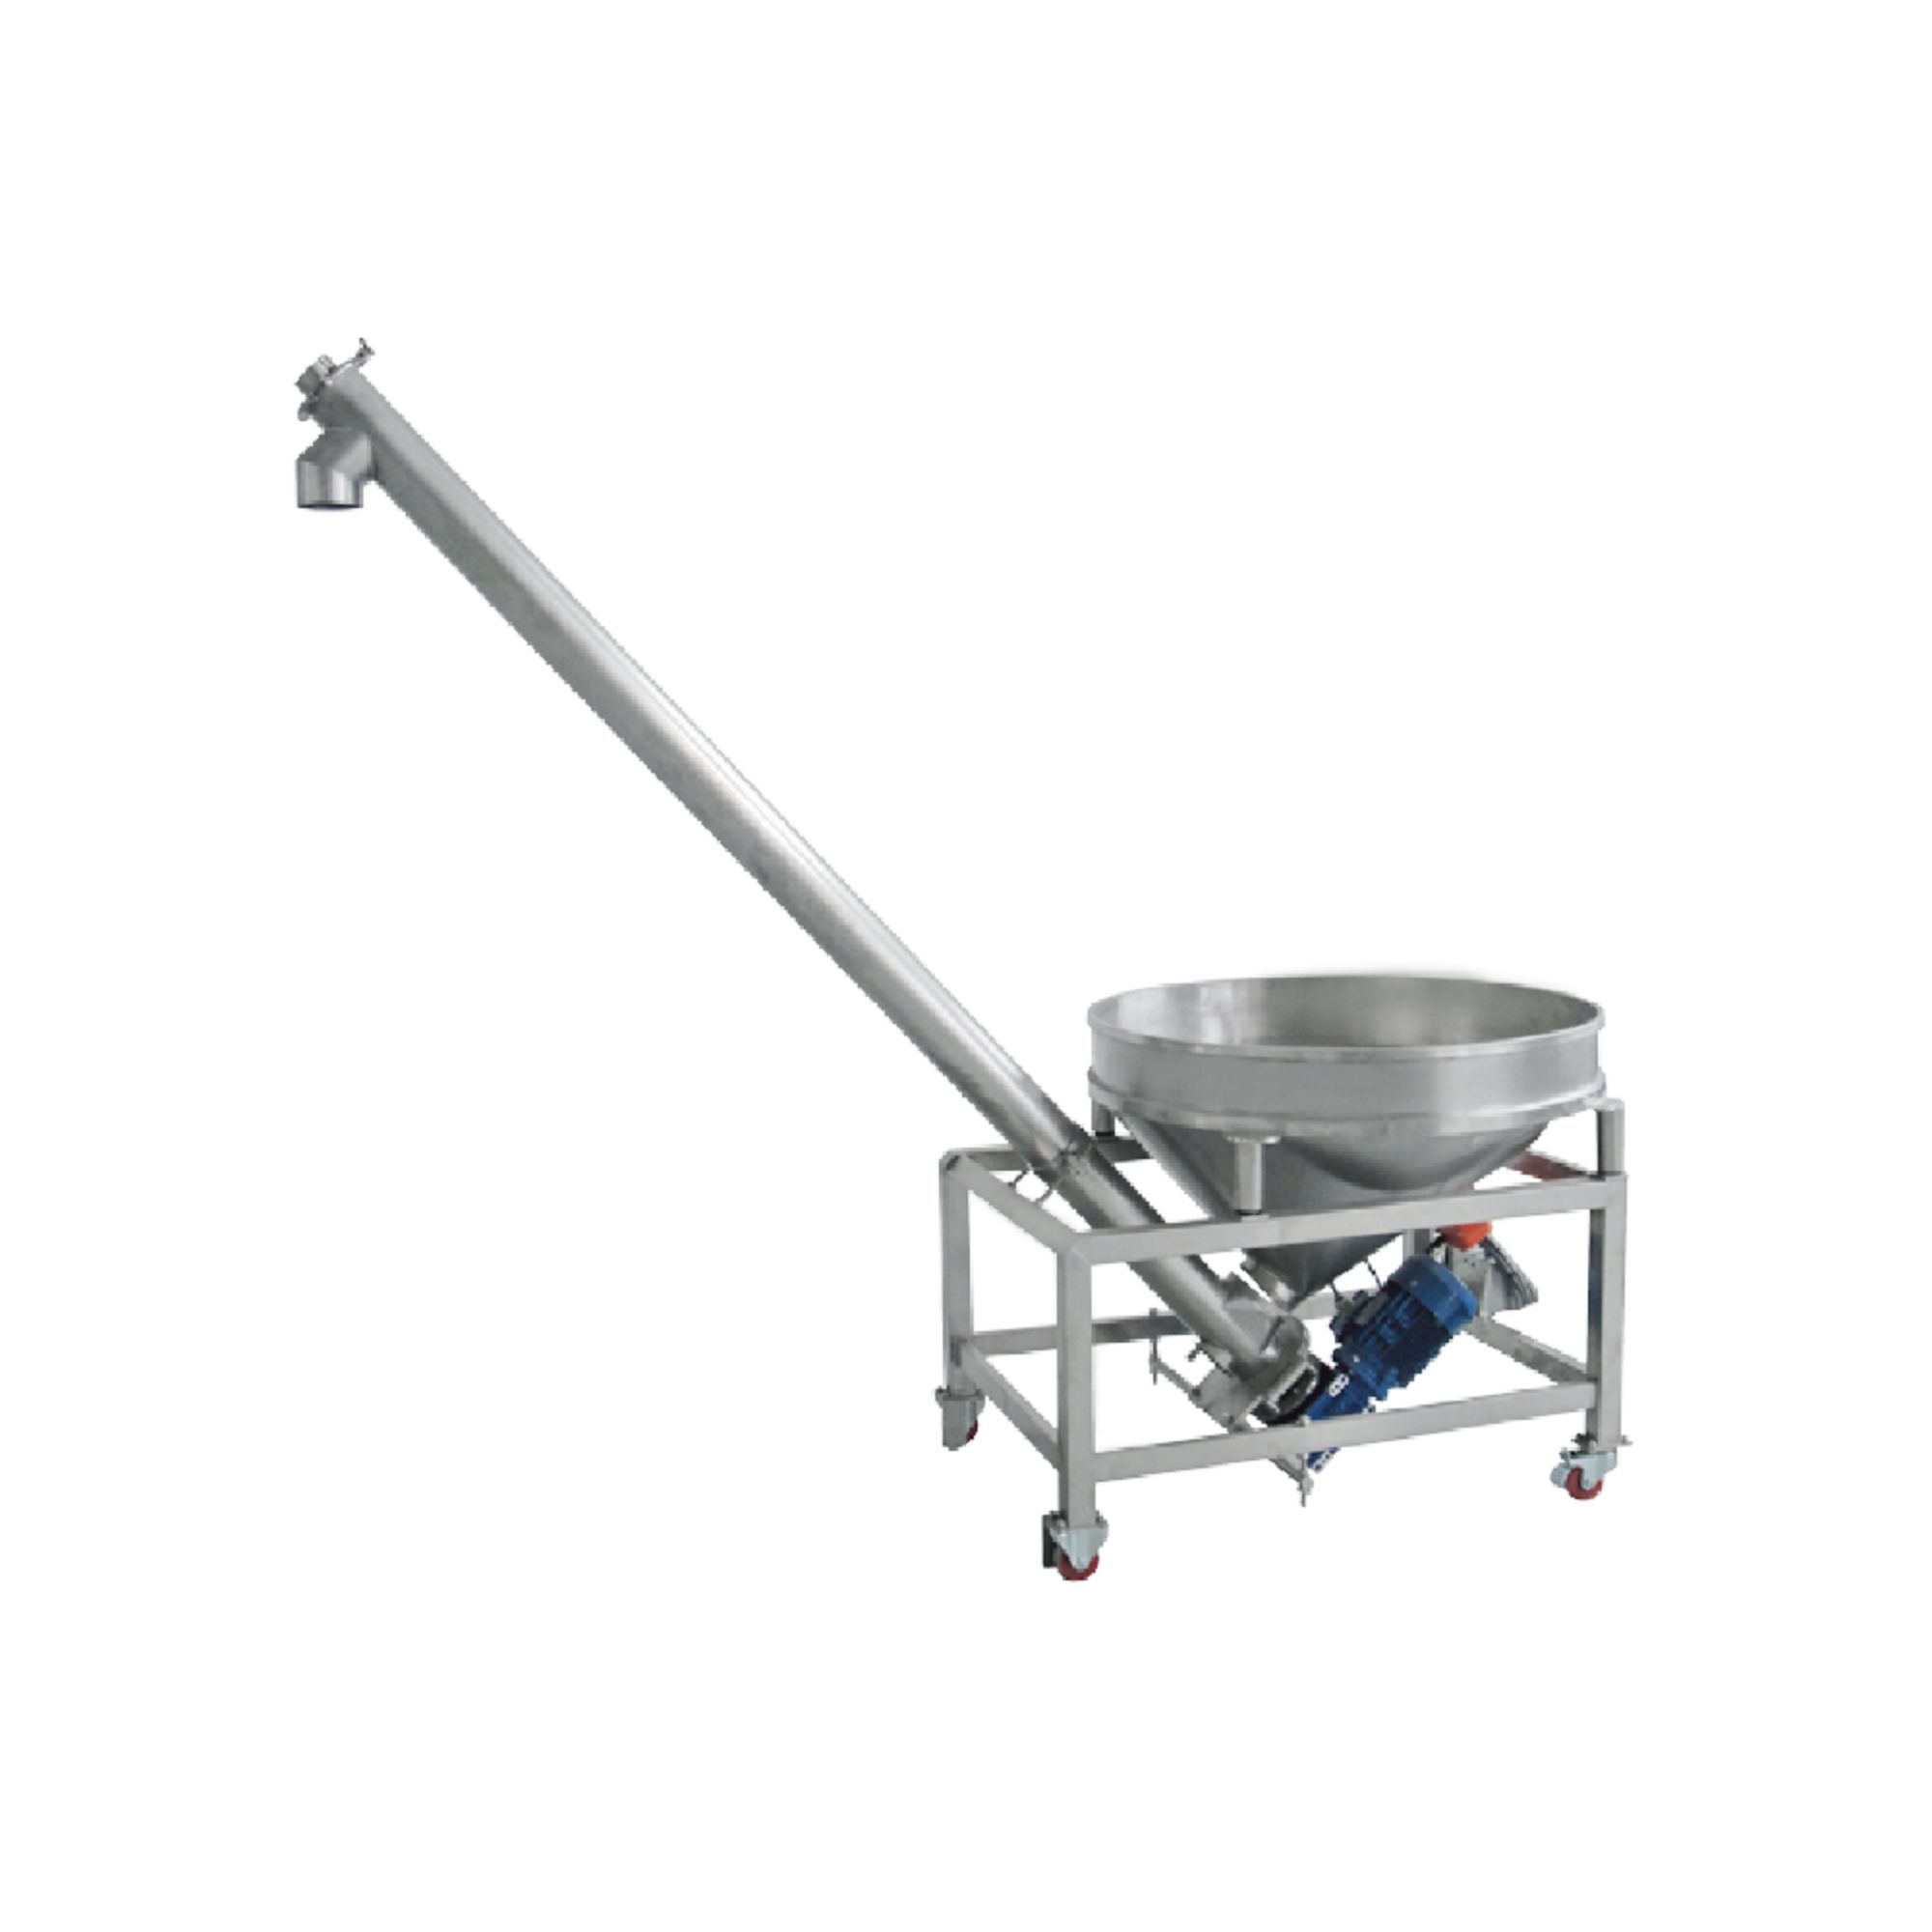
Big bag unloaders are versatile tools used across a range of industries, including food, pharmaceuticals, and new materials. In the food industry, they are essential for safely transferring bulk ingredients such as flour, sugar, and additives. The ability to handle these materials efficiently not only enhances productivity but also minimizes contamination risks, as many unloaders are designed with sanitary features. Additionally, considering the right Auxiliary Equipment can further improve the efficiency of your processes.
In pharmaceuticals, precision and cleanliness are paramount. Big bag unloaders used in this sector often incorporate advanced filtration systems to ensure that the powder materials remain uncontaminated during transfer. Buyers should confirm that the unloaders meet industry-specific regulatory requirements, such as those set by the FDA or EMA.
For new materials, such as advanced composites or specialty chemicals, big bag unloaders provide the flexibility to handle a variety of materials with different flow properties. It is essential to assess the material characteristics—such as moisture content and particle size—when selecting an unloader to ensure compatibility and optimal performance.
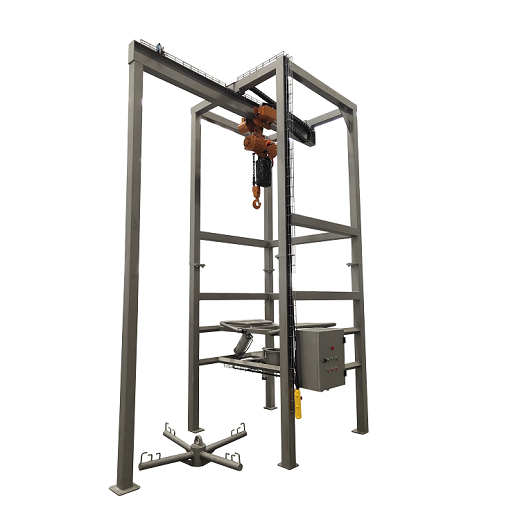
When considering bulk purchases of big bag unloaders, several cost factors should be taken into account. First, the initial purchase price may vary widely based on features, customization options, and manufacturer reputation. Buyers should compare quotes from multiple suppliers and assess the value of additional features that may enhance long-term efficiency.
Operating costs are another critical consideration. Evaluate the energy consumption of different models as well as maintenance requirements. Some unloaders may have higher upfront costs but offer lower operational costs due to energy-efficient designs or reduced wear and tear.
Additionally, consider the total cost of ownership, which includes shipping, installation, and potential downtime during the transition to new equipment. Discuss these aspects with your supplier to gain a comprehensive understanding of the financial implications of your purchase.
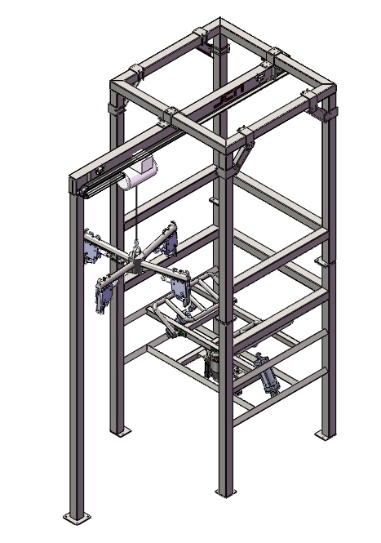
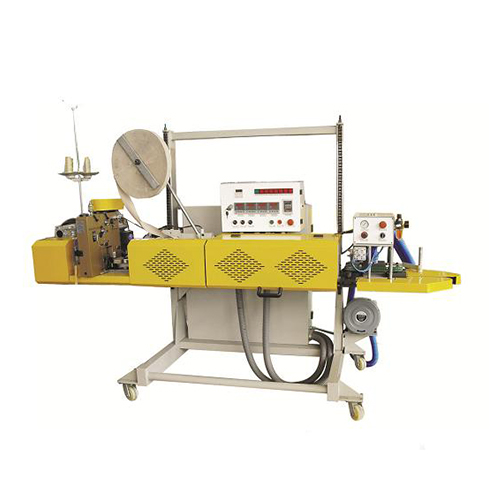
Sourcing reliable big bag unloaders begins with identifying reputable manufacturers known for their quality and industry expertise. Look for manufacturers that specialize in powder material handling, like JCN Co., Ltd., which offers high-tech solutions tailored for various industries, including Weighing Bagging Machine that are essential for accurate measurements in bulk handling.
Attend industry trade shows and exhibitions where you can interact with manufacturers, view their products, and gain insights into their capabilities. This direct interaction can help build trust and ensure that you are dealing with a credible supplier.
Furthermore, online platforms and industry directories can provide a list of potential suppliers. Always check customer reviews and case studies to ensure that the manufacturer has a proven track record of customer satisfaction and product reliability.
JCN a manufacturing company that occupies area of 30,000 square metres in Packing automatic machinecity Jiangsu province.And it has grown to become one of largest companies that designs, engineers, manufacturing and supply of modern powder material handling equipment.We remain committed to the idea creating value for our clients through quick communication, active cooperation, and continuous improvement of our behaviour.
JCN a manufacturer of powder handling equipment and equipment. Our primary products bag dumped, sieving, mixing, industrial weighing, auto-bagging as well as robotic palletising systems. They have been Sealing and packing machinewidely in food, new materials as well pharmaceutical industries, earning excellent reputation.
"JCN focusing on research and development food packaging equipment. We have taken on most advanced packaging Vertical mixertechnologies from overseas well as made improvements and advancements. We are available 24 hours day, 7 days a week for service,any questions machine operation just feel free to contact us."
JCN has been certified ISO 9001:2015 obtain CE certification as well as Packing automatic machineutility patent certificates.all our products are made entirely by factory. They are assembled and tested before delivery. Customers can also inspect the products verify they meet their needs.