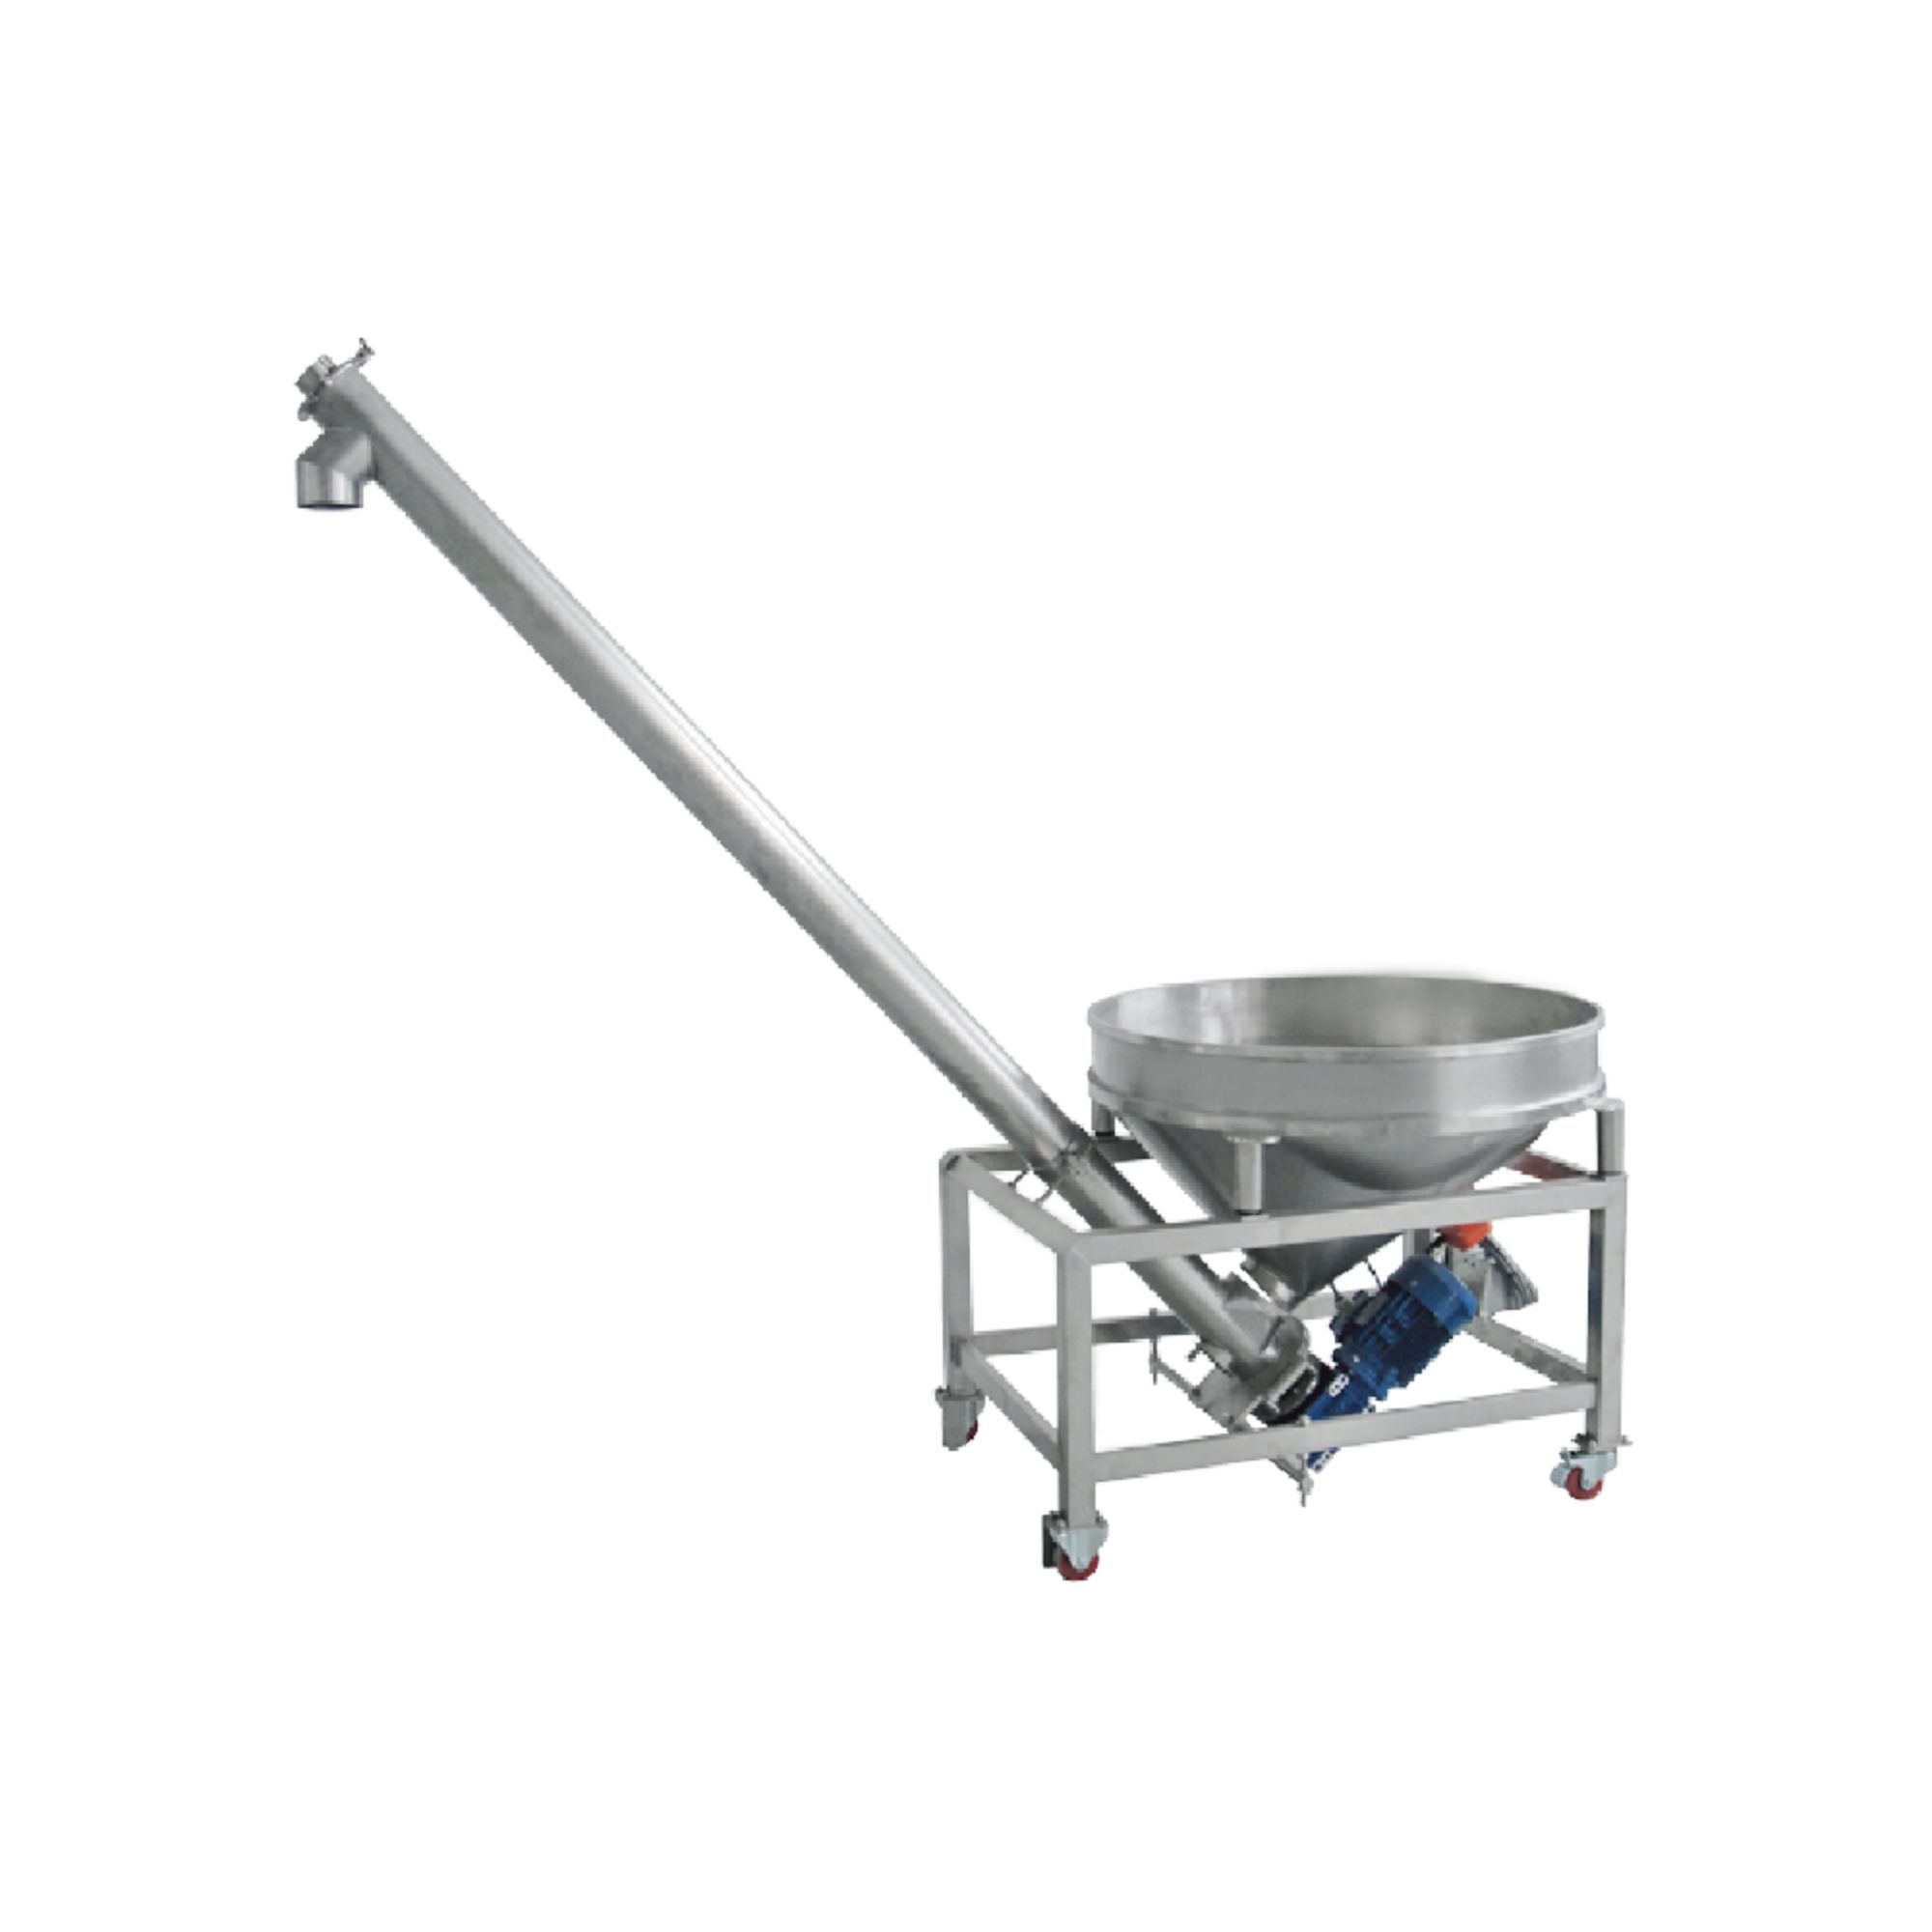
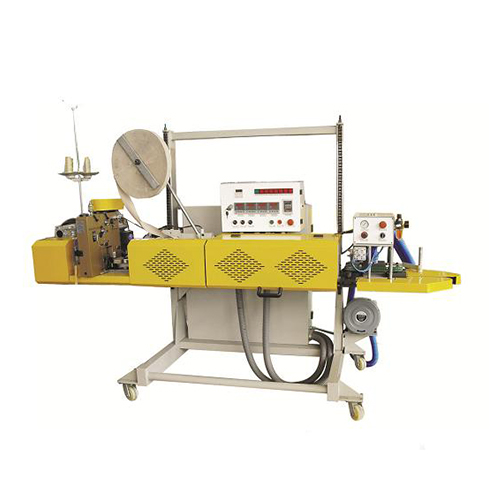
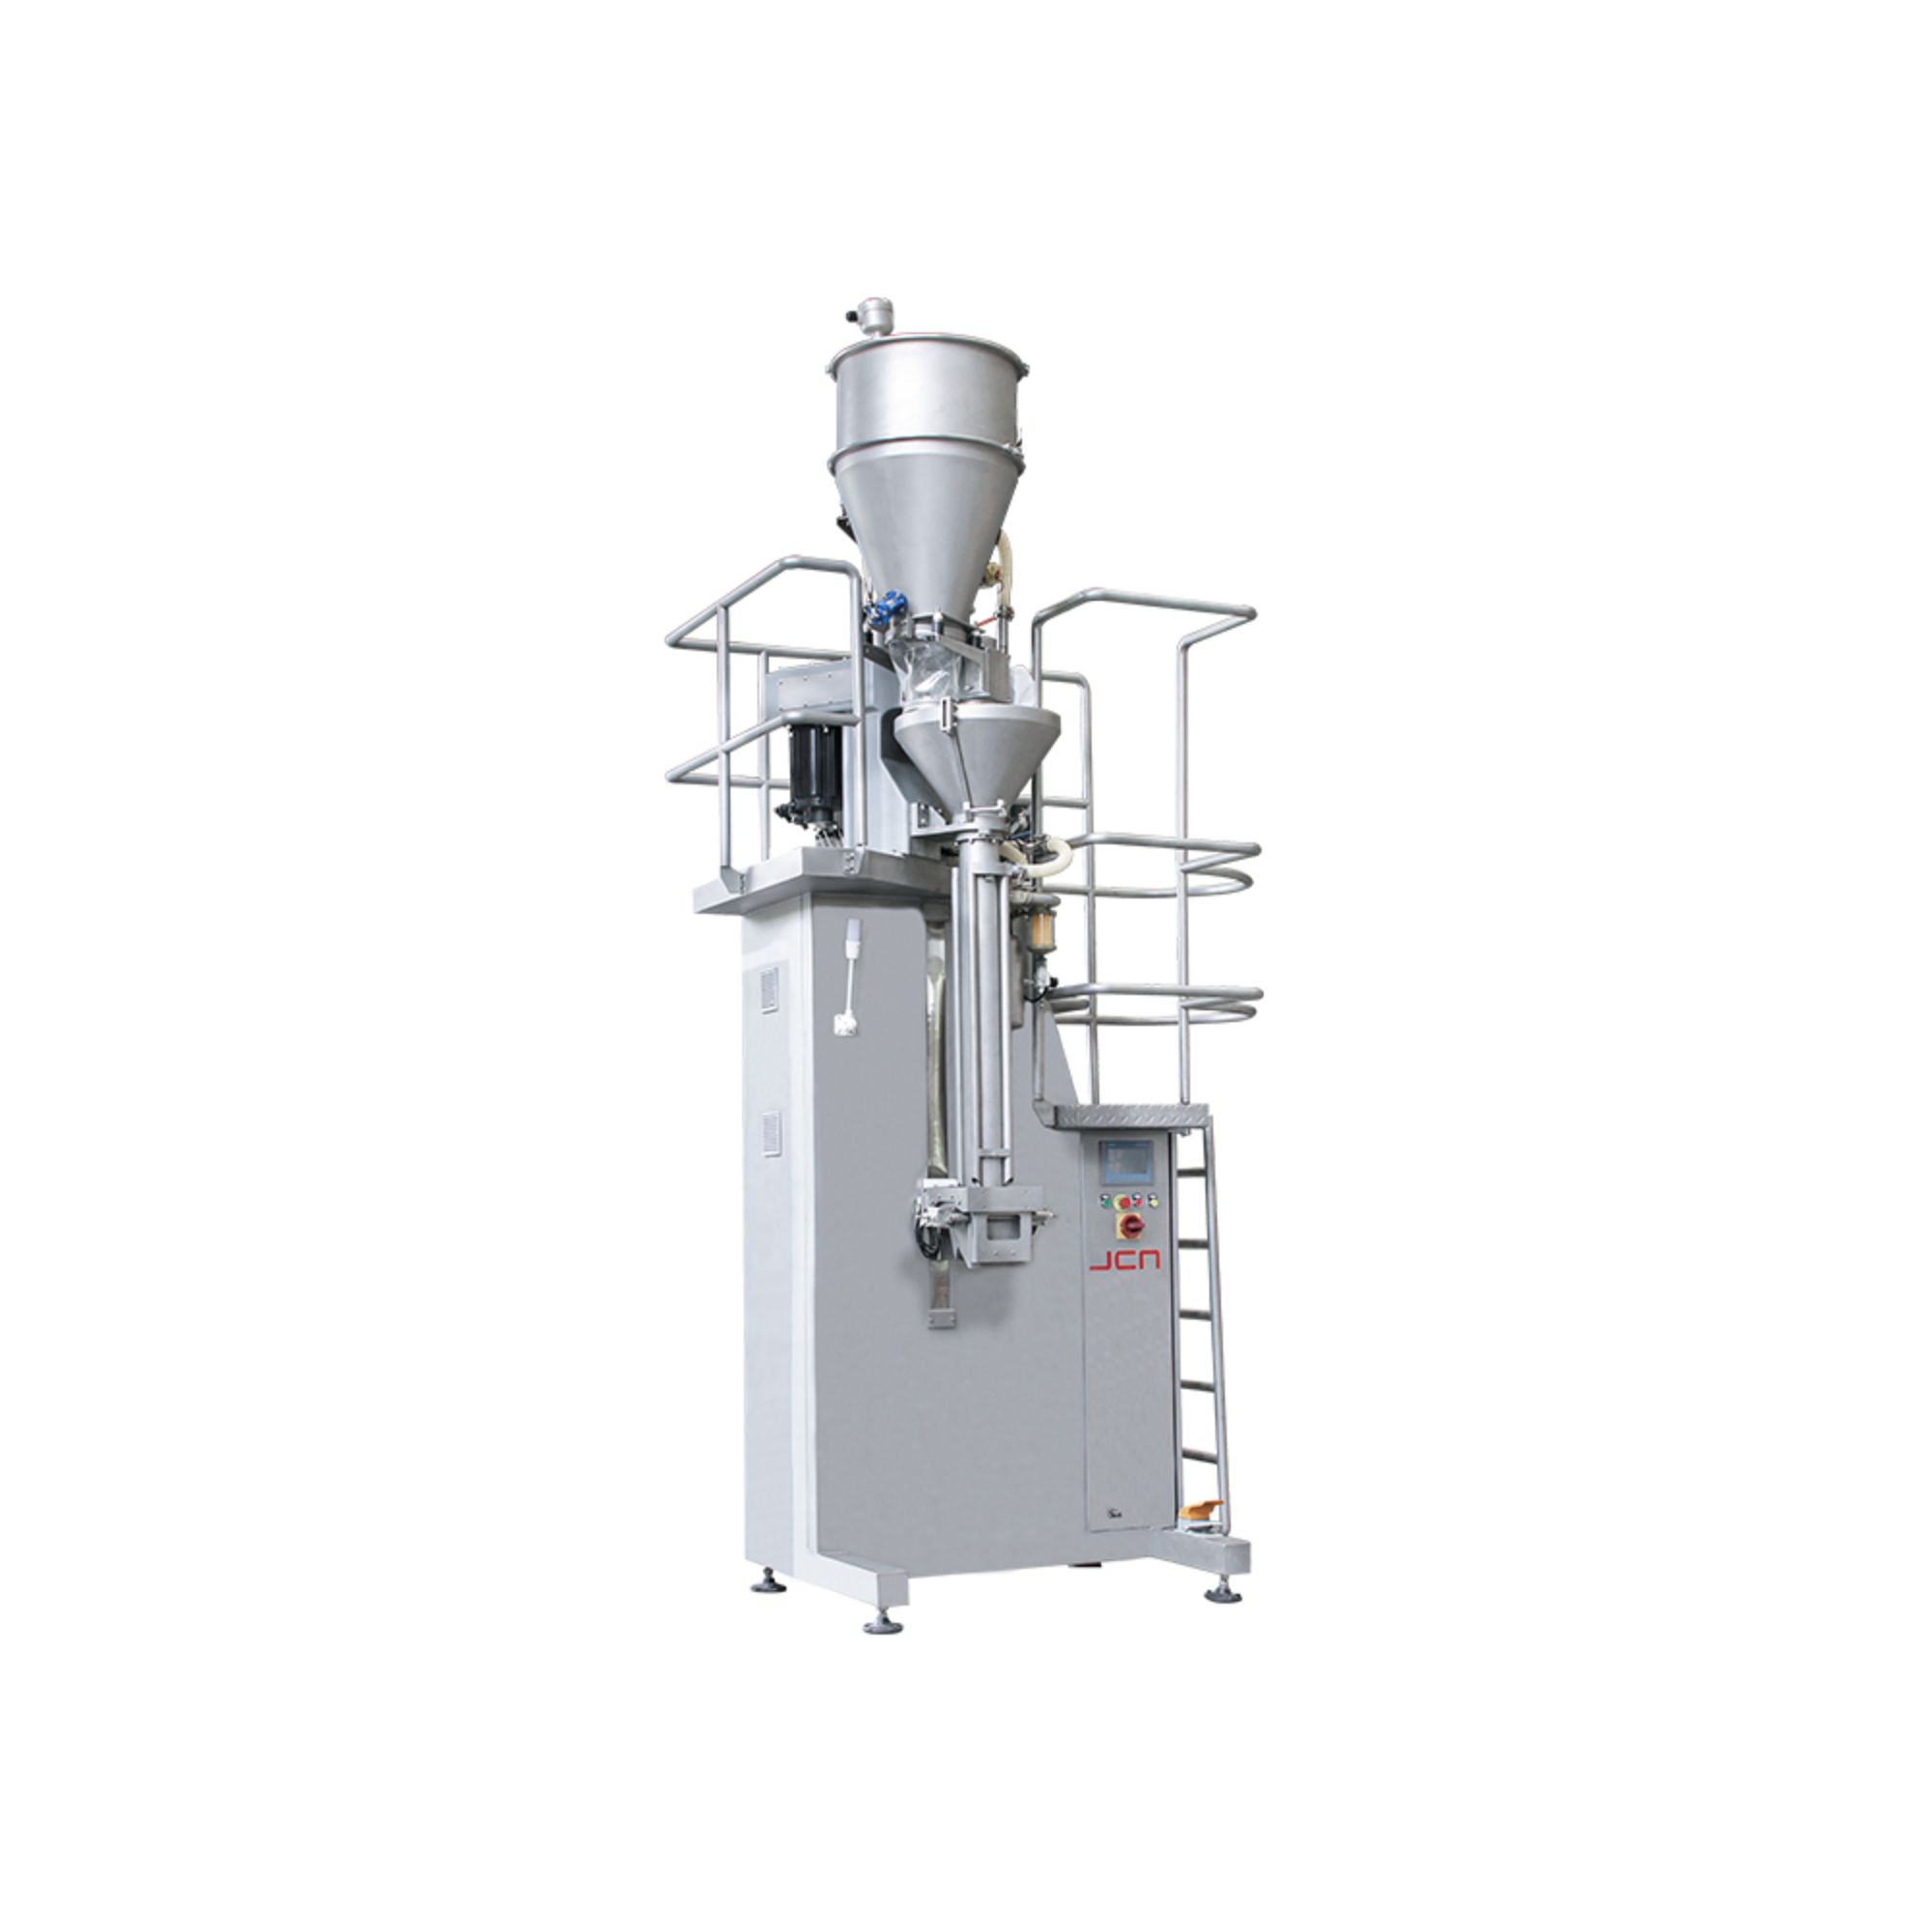
Bag dumping stations are essential equipment in manufacturing and processing facilities, designed to streamline the unloading of bulk materials from bags. As a B2B buyer, your main concerns typically revolve around efficiency, reliability, and compliance with industry standards. This article will provide valuable insights into the features and benefits of bag dumping stations, quality control evaluations, installation guidance, their applications in food and pharmaceutical industries, and how to identify trusted suppliers.
Bag dumping stations are engineered to facilitate the safe and efficient transfer of bulk materials from bags into processing systems. Key features include:
Ergonomic Design: Many stations are designed with adjustable heights and tilting capabilities, reducing user strain and enhancing safety during operation.
Dust Control: Integrated dust collection systems help maintain clean working environments by minimizing airborne particulates, which is particularly crucial in sensitive industries like food and pharmaceuticals.
Versatility: These stations can handle various bag types and sizes, from woven polypropylene to paper bags, making them suitable for diverse applications. For example, they can be used in conjunction with a Bag Dumping Station to improve efficiency.
Robust Construction: Typically constructed from stainless steel or other durable materials, bag dumping stations offer longevity and ease of cleaning, ensuring compliance with hygiene standards.
Customizable Features: Options such as integrated scales for accurate weight measurement and automated bag cutters can be included to enhance operational efficiency.
Investing in a bag dumping station can lead to significant reductions in labor costs and material waste, optimizing your production process.
Quality control is paramount when selecting bag dumping stations. Here are critical factors to consider:
Material Specifications: Ensure that the materials used in construction meet industry standards for strength and corrosion resistance. Stainless steel is often preferred for its durability and ease of cleaning, especially in food and pharmaceutical applications.
Testing Procedures: Confirm that the manufacturer conducts thorough testing on their products, including load testing and performance evaluations. This ensures that the equipment can handle the required capacity without failure.
Certifications: Look for equipment that meets relevant industry certifications, such as ISO standards or CE marking, which indicate compliance with safety and quality regulations.
Supplier Reputation: Research the manufacturer's history and reputation in the industry. A trusted supplier will have a proven track record of delivering reliable and efficient equipment.
Post-Sale Support: Evaluate the level of customer service and technical support provided by the manufacturer, including warranty terms and availability of replacement parts.
By addressing these quality control aspects, you can ensure that your bag dumping station meets operational requirements and industry standards.
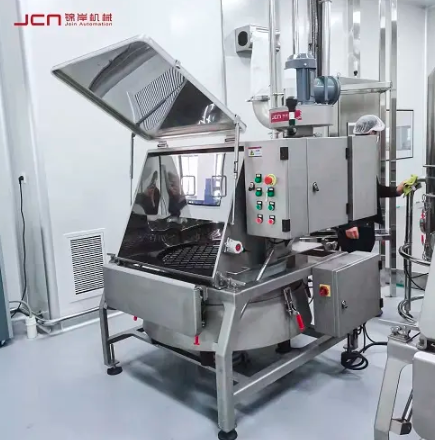
Proper installation of bag dumping stations is crucial for optimal functionality. Consider these guidelines:
Site Preparation: Before installation, assess the site to ensure adequate space and accessibility for maintenance. The area should allow for safe operation and have proper electrical and plumbing connections if necessary.
Leveling and Stability: Ensure that the station is leveled and secured to prevent tipping or movement during operation. Uneven surfaces can lead to operational inefficiencies and safety hazards.
Operator Training: Provide comprehensive training for operators on the equipment's functionalities, safety protocols, and maintenance routines to ensure smooth operation.
Integration with Existing Systems: Confirm that the bag dumping station is compatible with your current material handling systems, such as conveyors or hoppers. Proper integration minimizes disruptions in workflow.
Regular Maintenance: Establish a routine maintenance schedule to check for wear and tear, ensuring that all components are functioning correctly and safely.
By following these installation guidelines, you can enhance the efficiency and longevity of your bag dumping station setup.
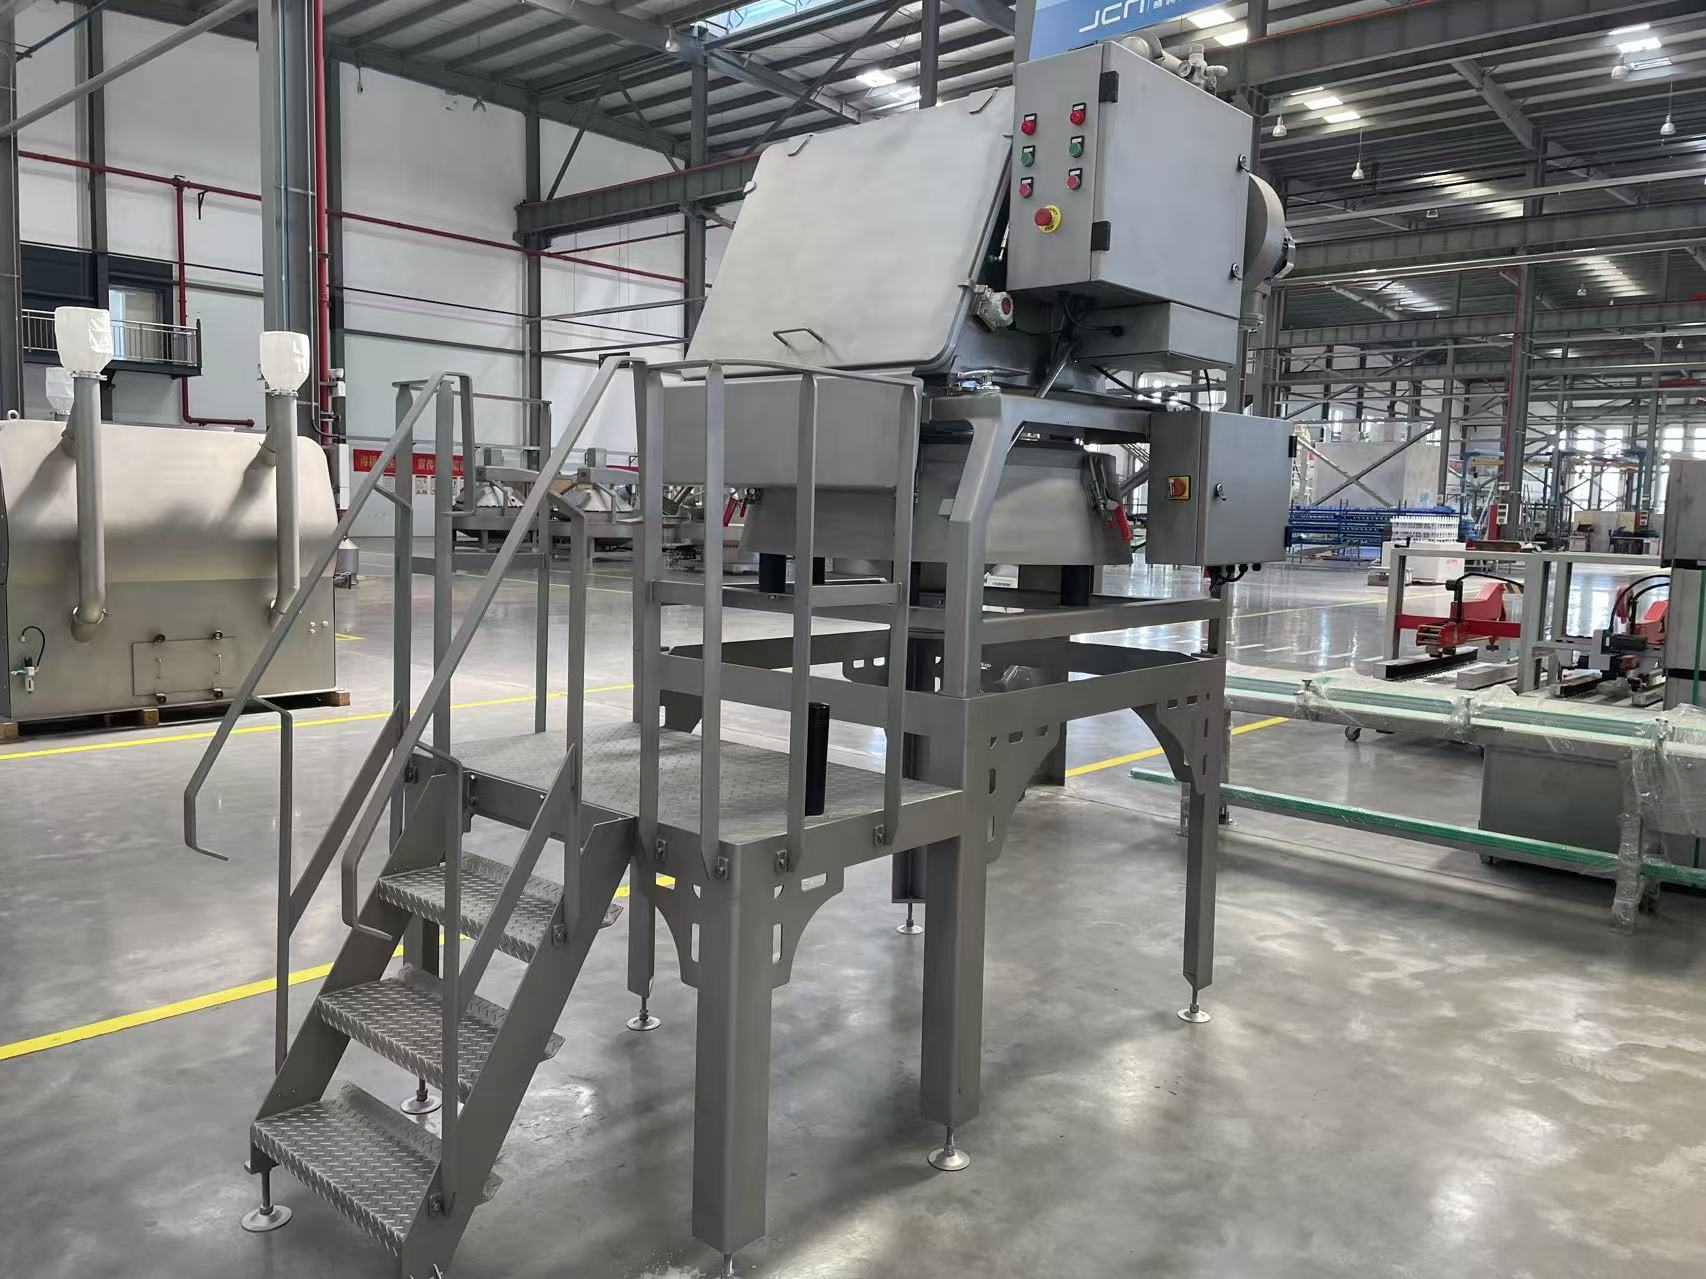
Bag dumping stations are widely used in the food and pharmaceutical sectors due to their ability to efficiently handle bulk materials while maintaining stringent hygiene standards. Key applications include:
Food Processing: In food manufacturing, bag dumping stations facilitate the transfer of ingredients such as flour, sugar, and other dry goods into mixers or hoppers. The dust control features are especially important in this industry to maintain a clean working environment.
Pharmaceutical Manufacturing: For the pharmaceutical industry, the stations are used to unload active pharmaceutical ingredients (APIs) and excipients. The materials must be handled with care to avoid contamination, making the dust collection and sanitary design features critical.
Chemical Processing: In addition to food and pharmaceuticals, bag dumping stations can be utilized in chemical manufacturing to safely handle powders and granular materials, ensuring compliance with safety regulations.
Recycling and Waste Management: These stations can also play a role in recycling operations, where bulk materials need to be transferred efficiently from bags to processing equipment. The integration of a Bulk Bag Filling Machine can enhance the process significantly.
Understanding these applications helps B2B buyers recognize the versatility and necessity of bag dumping stations in various sectors.
JCN has been certified ISO 9001:2015 have been awarded a CE certificate several utility patent certificates.And all our products 100% made in our factory,assembled and then tested before being delivered. Customers can also examine items to make sure that they in compliance with their Mixer vertical.
"JCN focus R and D food packaging machinery. have taken on the most advanced technology packaging machinery from Filling machine for powderand made improvements and innovation. We are available 24 hours a day, 7 days week for assistance, if you have any questions about machine operation simply get touch us."
JCN a manufacturing that covers 30,000 square meters Nantong city in Jiangsu province.And has become one of most prominent companies which designs, engineer, manufacturing and supply modern powder material handling equipment.We keep in mind principle of delivering value to our clients, through prompt communication, active Vertical mixerand constantly improving our methods of conduct.
JCN a manufacturer of powder handling equipment and equipment. Our primary products bag dumped, sieving, mixing, industrial weighing, auto-bagging as well as robotic palletising systems. They have been Filling machine for powderwidely in food, new materials as well pharmaceutical industries, earning excellent reputation.